7 Tips for Choosing the Right Palletizer
Choosing a palletizer is not just a matter of matching a machine to a target rate. The right system must handle your case sizes, product mix, shift patterns, and available floor space. A line running uniform cartons has different needs from one switching between several package formats. Small details count. Case stability, pallet dimensions, and the location of the infeed can all affect reliable operation. A fast machine may still become a bottleneck if upstream equipment cannot keep pace.
These seven tips will help you assess practical requirements before comparing palletizer options. Consider throughput during normal production, not just a supplier’s best-case figure. Review changeover steps, guarding, controls, maintenance access, and how the machine will connect with conveyors and wrapping equipment. Ask for clear performance assumptions and a demonstration using representative products when possible. A spreadsheet alone can mislead. Site conditions and day-to-day operator needs matter, too. It is also worth questioning whether full automation is appropriate; a simpler configuration may better suit a smaller or frequently changing operation. No single design fits every facility. By weighing capacity, flexibility, footprint, support, and long-term operating costs, you can make a more informed choice and identify trade-offs before installation.
Define the Load Profile: Cases per Minute, SKU Count, and Shift Peaks
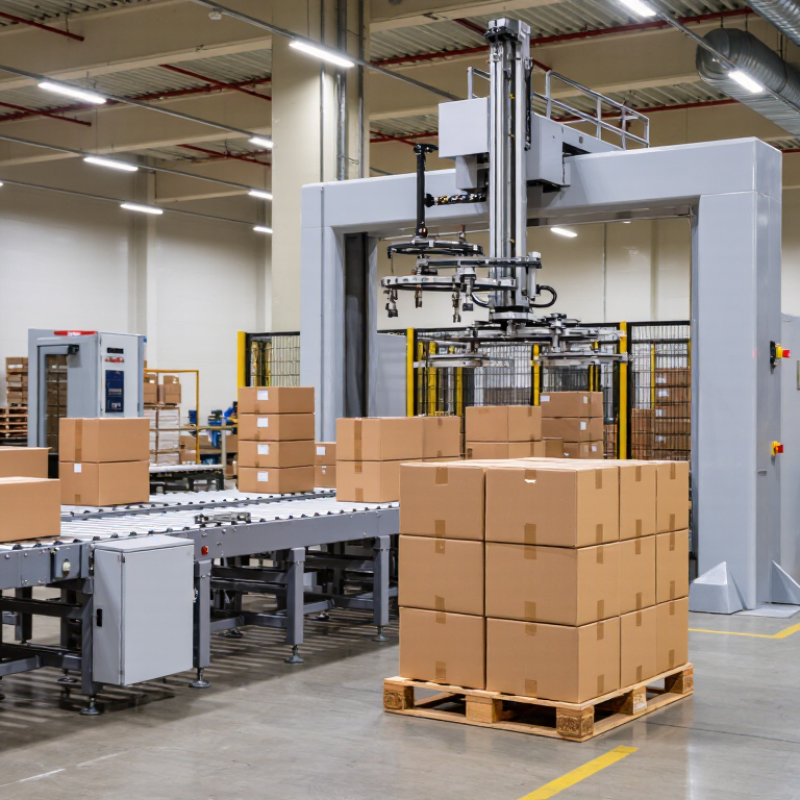
A palletizer should be sized around the load profile your line actually produces, not just its advertised average. Record cases per minute during normal production, changeovers, and short stoppages. Numbers matter. A line averaging 20 cases per minute may briefly reach 30 when upstream equipment releases accumulated cartons. Those bursts can overwhelm a system that looks adequate on paper.
Count the SKUs that will run through the cell and note how often case dimensions change. One stable carton size is simpler to handle than several sizes with different heights, weights, or stacking patterns. Include pallet patterns, too: a lightweight case may need a different arrangement from a dense one to keep the load stable. Check the data against real production records; estimates from a quiet shift can be misleading.
Peak hours matter. Compare demand across shifts, including breaks, planned maintenance, and seasonal surges. A short peak may call for accumulation space rather than a faster palletizer, but that depends on available floor space and upstream flow. Leave some capacity margin, yet avoid choosing equipment based on a rare, extreme rate. That estimate can still be wrong. Revisit the profile with operators and maintenance staff, since they often know which peaks repeat and which occur only after an unusual disruption.
Match Pallet Size: ISO 6780 Includes 1,200 × 800 and 1,200 × 1,000 mm
When selecting a palletizer, match its working envelope to the pallets moving through your facility. ISO 6780:2003 specifies standard pallet dimensions, including 1,200 × 800 mm and 1,200 × 1,000 mm. The first footprint is 200 mm narrower. That difference affects layer patterns, conveyor guides, and where cartons sit near the pallet edge. Small mismatch. A pallet’s nominal size is only the starting point; confirm actual dimensions and condition with samples from your supply.
Before approving equipment, test both sizes with real loads. Check fork-entry direction, conveyor width, transfer clearances, and the stability of the finished stack. A 1,200 × 1,000 mm pallet may need a wider infeed, while the 1,200 × 800 mm format can change carton placement across each layer. Ask for a trial using typical cases, including the light or awkward ones. Measure overhang, too. It is easy to trust a drawing and miss a few millimeters in worn pallets or packed cartons. ISO 6780 offers a dependable dimensional reference, but it cannot replace checks against your site’s pallets, loads, and handling equipment.
Calculate Payload from Product, Packaging, Slip Sheets, and Pallet Mass
A palletizer’s payload is not just the weight of the products.
Count every item lifted in one cycle: packed cases, slip sheets, and the pallet when it is carried with the load. Use the mass of a finished case, not the product alone, so cartons, trays, and wrapping are included without being counted twice. Small details add up.
For example, a pallet with 96 cases at 8.2 kg each carries 787.2 kg in cases. Add seven slip sheets at 0.6 kg each and a 25 kg pallet, and the total reaches 816.4 kg. These figures are illustrative; actual weights can vary between batches. Weigh a complete, representative load when possible, and account for heavier packaging or damp pallets if they occur in normal operation. A neat spreadsheet can still be wrong if its inputs are guesses.
Check how the palletizer’s rated payload is defined.
Some ratings include the gripping tool; others list tool mass separately. Confirm the combined load stays within the machine’s limits, including during acceleration and stopping. Leave suitable capacity for routine variation, rather than sizing to one unusually light pallet. The margin should reflect measured variation and the equipment specification, not a convenient round number.
Compare Robotic and Conventional Palletizers by Rate and Changeover Needs
A palletizer’s rated speed matters only if it matches the line’s real output. Compare cases per minute with the fastest sustained rate upstream, not a brief peak. Conventional palletizers can suit steady, high-volume runs with a small number of fixed patterns. Robotic palletizers may handle more pattern variation and product changes with less mechanical reconfiguration. Neither option is automatically faster. Case size, layer stability, infeed spacing, and downtime all affect actual throughput. Rate alone misleads.
Changeover needs can tip the decision. If operators switch between several case sizes or pallet patterns each shift, ask how recipes are selected and how long a verified change takes. A robotic system may simplify pattern changes, but grippers, safety checks, and product trials still take time. Conventional equipment may need physical adjustments, yet familiar, infrequent changes can be straightforward. Ask suppliers to demonstrate your actual cases and patterns, then record changeover time and good pallets per hour. A spreadsheet can make this look cleaner than it is. Allow for jams, restocking, and operator response; the test should reflect a normal shift, not a perfect one.
Verify Cell Safety Against ISO 10218 and ISO 13849-1
A palletizer may look safe during a quiet demonstration, but production changes the picture. Boxes shift, operators clear jams, and forklifts pass nearby. Ask how the safety design was assessed against the applicable editions of ISO 10218 and ISO 13849-1. These standards address industrial robot safety and safety-related control systems; they are not a substitute for a site-specific risk assessment.
Inspect the cell layout, not just the robot. Check reach-through gaps, fence height, access gates, and the space around pallet loads. Ask what happens when a gate opens, an emergency stop is pressed, or power returns after an outage. Safety functions should be designed to the required performance level, then validated with documented tests. Small gaps matter. So does reset location: an operator should not restart equipment without seeing the hazard area.
Request risk-assessment and validation records, and confirm who maintains them after installation changes. A new gripper or altered pallet pattern can change the risk. Test realistic tasks, including jam clearing and replenishment, with trained personnel and safe procedures. A checklist helps, but it can miss awkward workarounds. I would also ask operators where they feel tempted to reach inside; their answers may reveal a design flaw that a clean factory test never showed.