How to Choose the Best Case Packer Manufacturers in 2026
Choosing the right case packer manufacturers in 2026 means looking beyond machine speed. A line may run smoothly during a factory demonstration, then struggle with your actual cartons, products, or shift patterns. Start with the details that shape daily performance: pack styles, case dimensions, changeover frequency, required output, and available floor space. Bring real samples to supplier discussions. Small differences in flap strength or product spacing can affect reliable case forming and loading.
Ask manufacturers to explain how they test throughput, manage changeovers, and support equipment after installation. Request references from facilities with similar products and operating conditions. Review service coverage, spare-parts availability, operator training, and integration experience with your existing conveyors and controls. Useful evidence includes a documented acceptance test, clear performance assumptions, and a defined process for handling technical issues. Impressive numbers alone are not enough.
A careful comparison should also account for total cost of ownership, including installation, maintenance, and expected downtime. Automation can reduce repetitive handling, but it will not fix every packaging problem. Sometimes the case design needs work. That part is easy to overlook. Be cautious when proposals promise results without explaining the assumptions behind them. No supplier can predict every production interruption. The best choice is usually a manufacturer willing to discuss limitations, verify fit with your products, and support the system after startup. Use these criteria to compare options with confidence, while leaving room for a practical site assessment before committing.
Define Case Size, SKU Range, and Required Throughput Before Comparing Suppliers
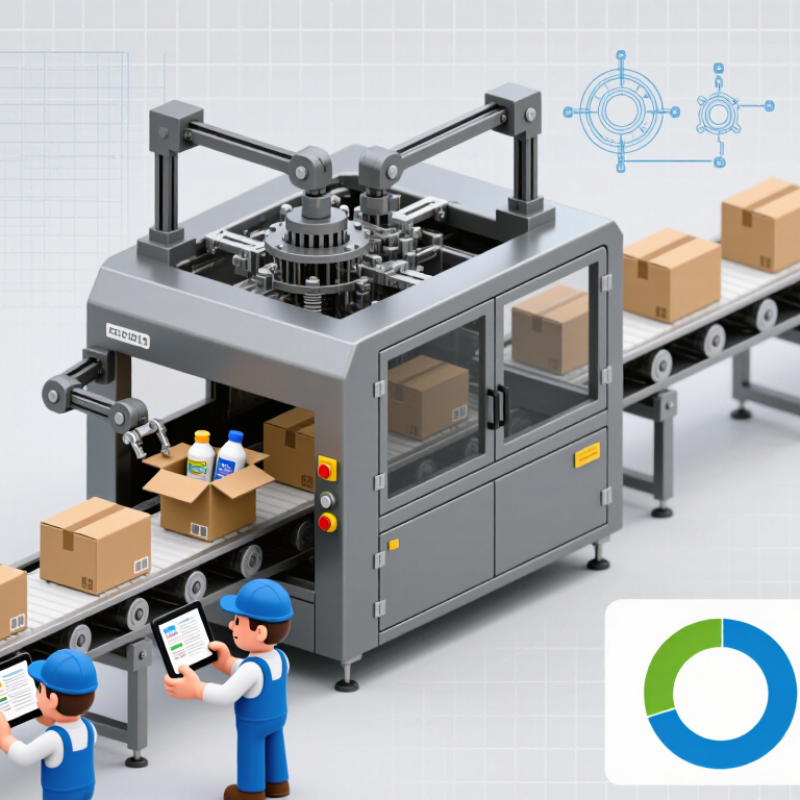
Before comparing case packer manufacturers, document the products and cartons your line must handle. List each SKU, case dimensions, product orientation, pack pattern, and changeover frequency. Include minimum and maximum sizes, not only the most common carton. A line running one stable format may need a simpler system than one switching between bottles and pouches. Small details matter. Measure physical samples; drawings can miss flap overlap or board variation.
Set required throughput as good packed cases per minute under normal operating conditions, not a brief peak speed. Record shifts, upstream supply gaps, and downstream limits. Ask suppliers to test your products, cartons, and pack patterns. Confirm changeover time, adjustment tools, staffing needs, utilities, footprint, and service support. Request clear acceptance criteria for a performance test. Quotes sometimes rely on assumptions. Check them carefully. A target speed may not be realistic across every SKU, and I would rather uncover that before installation than explain it afterward.
Tips: Bring several carton samples, including the smallest and largest. Share a realistic production schedule, not just the ideal one. Note any awkward formats, even if they account for few orders.
Compare Rated Speed and OEE: Availability × Performance × Quality
A case packer’s rated speed is a ceiling, not a promise. Compare it with good cartons per scheduled minute, then check OEE: availability × performance × quality. ISO 22400-2 describes OEE through these three factors, making it more useful than a nameplate figure alone. For example, a machine rated at 30 cases per minute, with 90% availability, 80% performance, and 98% quality, produces about 21.2 good cases per scheduled minute. Small losses add up.
Ask manufacturers to run your carton sizes, product mix, and changeover sequence. Record micro-stops, jams, replenishment pauses, and damaged cartons—not just steady-state cycles. A fast test on one perfect carton can flatter the result. A little skepticism helps. Request the raw time log and agree whether planned cleaning and changeovers count as scheduled production time; otherwise, OEE comparisons are not like for like.
Deloitte’s 2024 Smart Manufacturing Survey of 600 executives found that 86% expect smart manufacturing to be a primary driver of competitiveness within five years. That makes exportable downtime and reject data worth requesting—not vague efficiency claims. Still, software cannot fix poor carton presentation. Compare OEE over a representative shift, and document acceptance targets. Operators may need time to settle the line.
Check Machine Risk Controls Against ISO 12100 and ISO 13849-1 (PL a–e)
When choosing case packer manufacturers in 2026, ask how they apply ISO 12100 to the actual machine, not just a standard drawing. A case magazine, carton pusher, and tape head each create different access and pinch hazards. The International Labour Organization’s 2023 global estimates report 2.93 million work-related deaths and 395 million non-fatal work injuries annually. These figures cover all sectors, not case packing, but they show why risk controls deserve close scrutiny.
For each hazard, request the risk assessment and the required performance level, or PLr, for its safety function. ISO 13849-1 classifies performance levels from PL a to PL e. Check the achieved PL, safety-component details, and validation evidence for functions such as guard interlocks and emergency stops. Small details matter. Ask whether operators can reach the pusher during jam clearing, and whether doors remain locked until hazardous motion stops.
A neat certificate is not enough. A clean risk file can still miss awkward changeovers. Request practical demonstrations of foreseeable tasks, including cleaning and fault recovery, and compare them with the assessment. Confirm who validated the safety-related control system and whether the documentation matches the delivered machine. If the supplier cannot explain why a safeguard is adequate, treat that as an open risk—not a paperwork gap.
How to Choose the Best Case Packer Manufacturers in 2026
Check machine risk controls against ISO 12100 and ISO 13849-1 (PL a–e)
ISO 12100 provides the risk-assessment process used to determine the required Performance Level (PLr) for a safety function. ISO 13849-1 defines PL a–e by ranges of average probability of dangerous failure per hour (PFHd). Lower PFHd ranges indicate lower probability; the appropriate PLr depends on the assessed risk and should be verified for each safety function.
Assess Controls and Line Integration Using PackML (ISA-TR88.00.02)
When comparing case packer manufacturers in 2026, ask how each machine implements PackML, described in ISA-TR88.00.02. The standard provides a shared structure for machine states, operating modes, and status data. It does not guarantee easy integration. Request a live demonstration of transitions such as Execute, Held, and Aborted, using your cartons and operating conditions. That matters. Observe what the operator sees after a carton jam or gate event. Does the machine report a clear state and reason, or simply stop? Ask for the state model, tag list, and interface details before reviewing a proposal.
Then trace signals between the packer and neighboring equipment. Check command ownership, status updates, alarm identifiers, and restart behavior. Have your controls engineers test blocked and starved conditions, a format change, and recovery after a stop. Watch it. A PackML-capable machine may still need custom mapping to match your line’s controller or supervisory system. Ask the manufacturer to explain those mappings and show the equipment exchanging signals with a line simulator or your actual controls. A polished demonstration is not enough. One caveat: PackML aligns machine language, but it does not define every site’s network design, safety requirements, or performance targets. Teams sometimes assume integration will be simple, then find inconsistent naming conventions during commissioning. Record those assumptions, and verify them before purchase.
Compare FAT/SAT Results, Changeover Time, and Lifecycle Service Support
A case packer can look reliable during a polished demonstration and still struggle with your cartons, operators, or production pace. Ask manufacturers to share FAT and SAT results from comparable applications. Review the test conditions, not just the pass mark. Were your actual carton dimensions, pack patterns, and target speeds used? Check records for jams, rejected cases, and recovery time. Small gaps matter.
During FAT, observe a full production run and a changeover between two real SKUs. Time the work from the last good case to the first approved case. Note which parts need tools, where settings are stored, and whether one operator can complete the steps safely. Paper passes are not enough. A tidy checklist may miss a stubborn guide rail or confusing screen prompt. It happens.
SAT should confirm performance at your site, with your materials and utilities. Set acceptance measures before installation, including sustained output and restart behavior after a minor fault. Then examine service support beyond commissioning. Ask how quickly technicians respond, which spare parts are stocked, and whether remote diagnostics are available. Request a sample maintenance schedule and training plan. If answers stay vague, record that concern; it may reveal more than a sales presentation. Check whether support covers software updates and future format changes, not only mechanical repairs.